Plastic crusher blade holder design affects how knives are supported, aligned and serviced, but no geometry should be judged by one energy-saving claim. A stepped or staggered cutting arrangement may change the sequence of material contact; its value depends on the feed, rotor, chamber, drive and maintenance requirements.
I recommend reviewing the complete load path and asking for evidence under defined material conditions. Buyers should compare stable operation, usable output and service access together.
Match Cutting Geometry to the Actual Feed
| Design factor | Purchasing question | Evidence to request |
|---|---|---|
| Cutting sequence | How does material contact the knives? | Rotor drawing or clear operating demonstration |
| Holder support | How are cutting loads transferred into the rotor? | Construction details and inspection points |
| Knife position | How is alignment maintained after service? | Reference surfaces, adjustment and measurement method |
| Fasteners | How are they accessed and controlled? | Tool access and approved tightening procedure |
| Material release | Can irregular feed move without persistent bridging? | Representative material trial and chamber observation |
| Wear protection | Which surfaces are replaceable or repairable? | Parts drawing and service boundary |
Review the Load Path Instead of a Percentage Claim
Progressive contact can distribute cutting events differently from full-width contact, but the result cannot be separated from knife sharpness, clearance, rotor speed, flywheel effect, motor control and feed consistency. An unloaded power figure or an undefined internal test does not prove production efficiency.
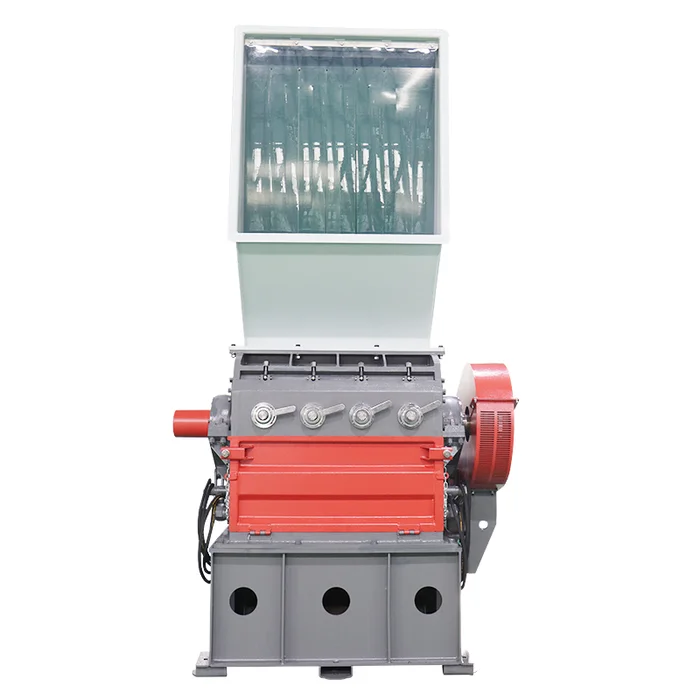
Ask the supplier to use the same representative feed, screen, knife condition and test duration for any comparison. Record usable output, motor-load trend, recirculation, heat, vibration and the condition of the material after the trial. The WHC800/450 industrial plastic crusher can be assessed against this evidence framework for the intended application.
Treat Maintainability as Part of Rotor Design
- Confirm access to every knife and fastener.
- Identify the reference used to set alignment and clearance.
- Review how damaged holders or threads are inspected.
- Ask which rotor parts are replaceable and which require factory repair.
- Check cleaning access around stepped or recessed surfaces.
- Include spare knives, fasteners and measuring tools in the service plan.
A holder that performs well but is difficult to inspect can create hidden maintenance risk. The buyer’s evaluation should include both the cutting task and the full service cycle.
Frequently Asked Questions
Does a stepped blade holder always use less energy?
No. Energy use depends on the complete machine, material, screen, feed rate and knife condition. Verify performance under agreed test conditions.
What is the difference between a blade holder and the blade material?
The holder supports and positions the knife; the knife material and heat treatment determine other wear and toughness characteristics. Both require evaluation.
Why is rotor rigidity important?
The cutting assembly must maintain the intended relationship between rotating and fixed knives under the specified load and service conditions.
How can alignment be checked after blade service?
Use the reference surfaces, measurement method and clearance values approved for the specific machine design.
What should be included in a blade-holder design review?
Send material, maximum feed size, contamination risk, capacity target, screen, duty cycle and maintenance constraints.
Request a Cutting-System Review
Use the AMIGE inquiry page to share representative material and operating requirements. We can review the rotor, holder, knives, screen and drive as one cutting system.